
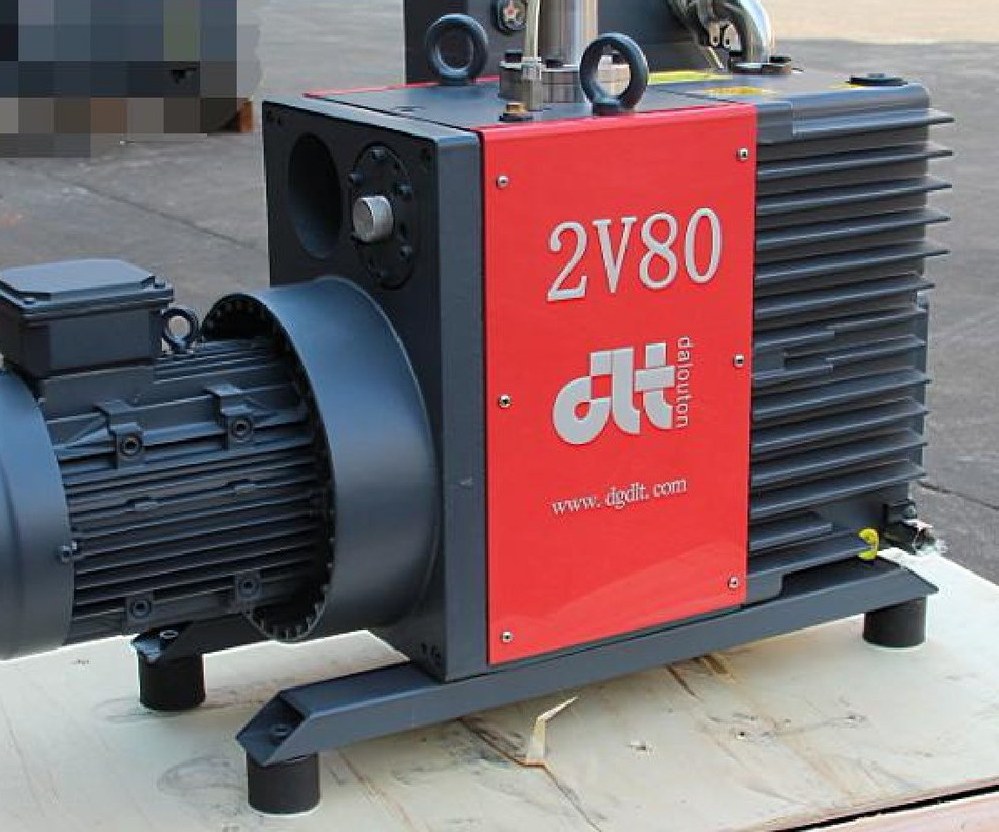
Duty: a chamber for coating, drying or inspection is pumped from atmosphere to a set rough pressure (commonly 10 to 20 kPa) each cycle, then a high-vacuum pump takes over. This stage moves the largest volume of gas, so an undersized pump stretches the cycle.
Approach: estimate the pump-down time as t = (V / S) · ln(p₁ / p₂), where V is chamber volume, S the effective pumping speed, p₁ the starting pressure and p₂ the target. That gives an ideal figure: the actual pumping speed falls as pressure drops, and pipe bore, run length, bends and valves cut into the effective speed further, so real time runs longer than the calculation.
Configuration direction: for a 0.5 m³ chamber to 10 kPa, a V25/40 (40 m³/h) works out to a theoretical pump-down of roughly two minutes, but a small line bore or several bends clearly lengthens it. Where the chamber is large, or several chambers share one pump, move to a higher-capacity model or add a receiver to cover the peaks.
Points to watch: fit filtration and condensation ahead of the pump for process residue (dust, moisture, solvent vapour); leave cooling clearance when the pump sits inside the machine; watch body temperature in long continuous pumping.
This page describes a selection method, not a specific project record.